



What is a slew bearing? It is a large-diameter rolling-element bearing that lets one structure rotate on another while carrying axial load, radial load and tilting moment at the same time. You find it under cranes, excavators, solar trackers and turntables. Our Slewing Bearing range covers the main designs used in these machines.
A reliability team usually asks one question first: what does this damage tell us about why the bearing failed? Slew bearing failure analysis answers it by reading three things together: where the damage sits, what it looks like, and what the machine was doing when it appeared. Do that before you decide on repair or replacement, and you avoid fitting a new bearing into the same conditions that killed the old one.
Start With Where the Damage Sits, Not What It Looks Like
Many teams photograph a damaged raceway and search for a matching picture. That works poorly. Spalling from overload and spalling from contamination can look almost the same up close. Location separates them.
A slew bearing does not load its raceway evenly. Tilting moment pushes one side of the ring hard and unloads the opposite side. That creates a load zone, and the zone's position tells you the direction of the dominant load. Damage inside that zone points to load-related causes. Damage spread around the full circumference points to lubrication, contamination or corrosion.
In my 30 years of designing slewing bearings and slew drives, I have seen the same mistake repeatedly. A team inspects the worst-looking section and ignores the unloaded side. The unloaded side often holds the best clue, because it shows what the bearing looked like before the damage spread.
A field inspection sequence before disassembly
- Record the machine's duty: load range, swing angle, rotation speed, hours and environment.
- Photograph the bearing in place, including seals, grease purge and mounting bolts, before any cleaning.
- Check rotation torque and tilting clearance around the full circle. Mark any tight or loose zones.
- Take grease samples from several points. Note color, metal particles and water content.
- Check bolt torque and look for fretting marks under the bolt heads and at the ring interfaces.
- Only then open the bearing. Map each damage area against the angular position of the load zone.
This sequence has a limit. It narrows the failure mode but cannot prove a metallurgical cause such as a material or heat treatment defect. That needs a sectioned ring and lab testing. Field work tells you where to send the sample.
Map Raceway, Rolling-Element, and Seal Damage Signatures to the Operating Conditions That Cause Them
The table below links what you see to the likely failure mode, the operating condition behind it, and the next check. Treat each row as a lead, not a verdict. Two signatures together are stronger evidence than one.
| Visible signature | Likely failure mode | Operating condition behind it | Check next |
|---|---|---|---|
| Flaking or spalling concentrated in the load zone | Rolling contact fatigue | Sustained overload, high tilting moment, or soft mounting structure; also normal end of life | Compare actual load and moment to the rated values; measure mounting flatness |
| Small craters, dull surface, spread widely | Surface fatigue from poor lubrication film | Wrong grease, long relubrication intervals, or fine abrasive in the grease | Grease analysis; relubrication records |
| Dents at ball or roller spacing on the raceway | Brinell (static overload) damage | Shock load while stationary, transport impact, or a collision with the boom parked | Review incident history; check whether dents sit at one angular position |
| Polished, scored raceway with abrasive particles | Abrasive wear | Dust or sand entering past damaged or poorly fitted seals | Inspect seal lips and grease for grit |
| Red-brown dust and shallow marks at contact points, limited angle | Fretting corrosion | Small oscillating motion with little rotation, such as tracking or positioning duty | Check the duty cycle and the relubrication method |
| Flat spots or blue-brown discoloration on balls or rollers | Overheating and lubricant breakdown | High duty cycle, heat soak, or lubricant starvation | Check temperature history and grease condition |
| Cracked, broken or worn cage or spacers | Shock, jamming, or misalignment damage | Debris between elements, severe moment, or deformed mounting surface | Look for debris marks; measure the mounting faces |
| Hardened, cracked or flattened seal lip | Seal aging | Heat, UV, ozone, or incompatible chemicals | Check the environment against the seal material |
| Torn or extruded seal | Seal mechanical damage | Over-greasing pressure, pressure washing, or installation damage | Review the greasing method and cleaning practice |
| Rust pitting along the raceway edge | Corrosion from water ingress | Failed seal or long idle periods in wet environments | Check grease for water; inspect seals and drainage |
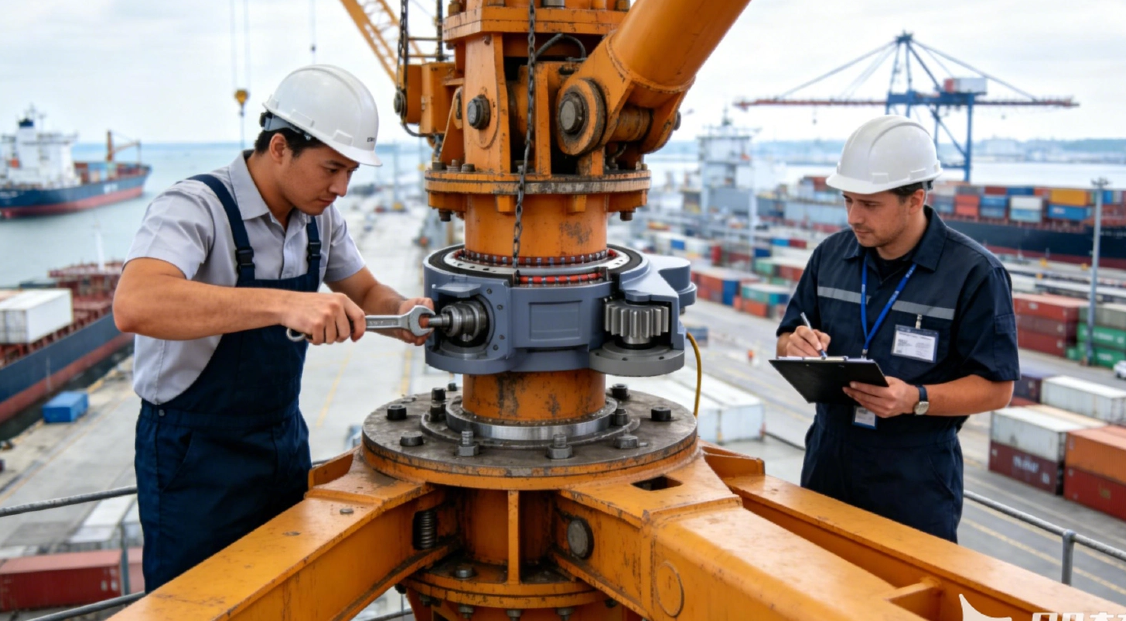
Two cautions apply. First, seal damage is often a cause rather than a result. A torn seal that let in grit explains the abrasive wear, so you must fix the seal path as well as the bearing. Second, a clean-looking raceway does not mean a healthy bearing. A bearing can show hard rotation from preload loss in the mounting structure while the raceway still looks fine.
Request Your Custom Slew Drive or Bearing Spec
Tell us your load, speed, and environment — receive a tailored 100–5000 mm slewing drive or slewing bearing proposal with 3D drawings within 24 hours.
How Load, Motion, Lubrication and Mounting Interact
Single parameters rarely explain a failure on their own. Each one changes how the others behave. The list below shows what each parameter affects and how misreading it changes your diagnosis.
- Load and tilting moment. They set the size and position of the load zone. A bearing rated for the axial load can still fail early if the moment is higher than assumed. Checking only the weight on the platform misses this.
- Rotation pattern. Continuous rotation spreads wear around the ring. Short oscillation repeats the same contacts, which favors fretting and local lubricant starvation. A bearing that suits one pattern may not suit the other.
- Lubricant and seals. Grease builds the film that separates the surfaces, and seals protect it. If the seal fails, the best grease still fails soon after. If the grease is wrong, the best seal will not save the raceway.
- Mounting stiffness and flatness. A flexible or uneven support deforms the ring under load. That shifts contact toward one edge and can mimic an overload failure. The bearing gets blamed when the structure is the cause.
- Material and heat treatment. We select ductile cast iron, alloy steel, stainless steel or forged alloy steel according to load, speed and environment. The right material for a corrosive site is not automatically right for a high-shock site.
The design type matters too. A three-row roller slewing bearing carries heavy moment on separate raceways, so the damage may be confined to one row. A single-row ball design shares all loads on one pair of contacts, so one overload event can show up across several signatures at once. Know the design before you read the raceway.
If the bearing is part of an integrated Slew Drive, add the gear mesh and housing seal to your inspection. Our slew drives offer protection up to IP66 and anti-corrosion ratings up to C4H. Those ratings describe the housing and sealing design, though, and do not replace correct greasing or a stiff mounting base.
Common Misreadings That Send the Diagnosis the Wrong Way
- "It rotates hard, so the raceway is damaged." Tight rotation can come from bolt over-torque, a warped mounting face or seal drag. Measure torque around the full circle and compare tight zones to the bolt positions.
- "The grease looks fine, so lubrication is not the issue." Color alone says little. Check for water, metal particles and whether the interval matched the duty cycle.
- "A cracked ring means a material defect." Cracks often start from fatigue at an overloaded zone or a stress point at the mounting. Without sectioning and lab tests, you cannot assign the cause.
- "We cleaned the bearing, then took photos." Cleaning removes debris patterns and fretting dust that carry the evidence. Photograph first.
- "Replace it and the problem is gone." If the load, seal path or mounting flatness has not changed, the new bearing will repeat the failure on a similar schedule.
When a manufacturing cause is possible, ask the supplier for the inspection trail. For our bearings, every unit passes CMM three-coordinate inspection and dynamic load testing, which is documented under our Slew Drive Quality Control process. Confirmed manufacturing defects are covered by free replacement, and the extended quality warranty runs for 2 years. This record helps rule defects in or out, but it does not cover damage from overload or contamination.
Applying the Evidence: Repair or Replace, and What to Send Us
Operating conditions point you to the signatures to check first. Consider three situations from our customer work. These cases describe the application context only, and the diagnostic notes are general engineering guidance.
- Mining excavators in Australia use our Double Worm Slew Drive (HWE21-94-25HR.1). Dust and shock loading are typical there. Check for abrasive wear, seal lip damage and Brinell dents first.
- Single-axis solar trackers in Brazil, Argentina and Chile use SP-I 0229 spur gear slew drives. The motion is small and repeated, and the equipment sits outdoors. Look at fretting marks, weathered seals and grease condition.
- Port cranes for a South Korean equipment maker use WEA9-62-25HR single worm slew drives, in a 20-unit repeat order with IP65 sealing. Cranes see heavy moment and wet air, so check load-zone fatigue and corrosion at seal edges.
Buyer's decision checklist: repair or replace
- Damage limited to seals and grease, raceway intact: resealing and regreasing may be enough. Confirm by checking tilting clearance.
- Localized Brinell dents with smooth rotation: monitor if the dents are shallow, but assess the risk if the machine is safety-critical.
- Spalling in the load zone, loose clearance, or cage damage: plan replacement. Fix the cause before fitting the new unit.
- Damage matches an operating condition you cannot change, such as higher moment: consider a larger or Customized Slew Drive instead of a like-for-like swap.
To speed up the review, send these items to our engineers at Luoyang Slewring Bearing Co., Ltd.: the model or drawing number, photos taken before cleaning, duty cycle and load data, grease type and interval, the environment, and the mounting structure details. We respond to technical questions within 48 hours and can return a technical proposal within 24 hours. Standard products start at a 1-set MOQ, and customized products at 5 sets.
Slew bearing failure analysis will not give you certainty from a photo alone. It will give you a ranked list of causes, a short list of checks, and a clearer basis for deciding between repair and replacement.
Request Your Custom Slew Drive or Bearing Spec
Tell us your load, speed, and environment — receive a tailored 100–5000 mm slewing drive or slewing bearing proposal with 3D drawings within 24 hours.
 WhatsApp

 +8613903880726